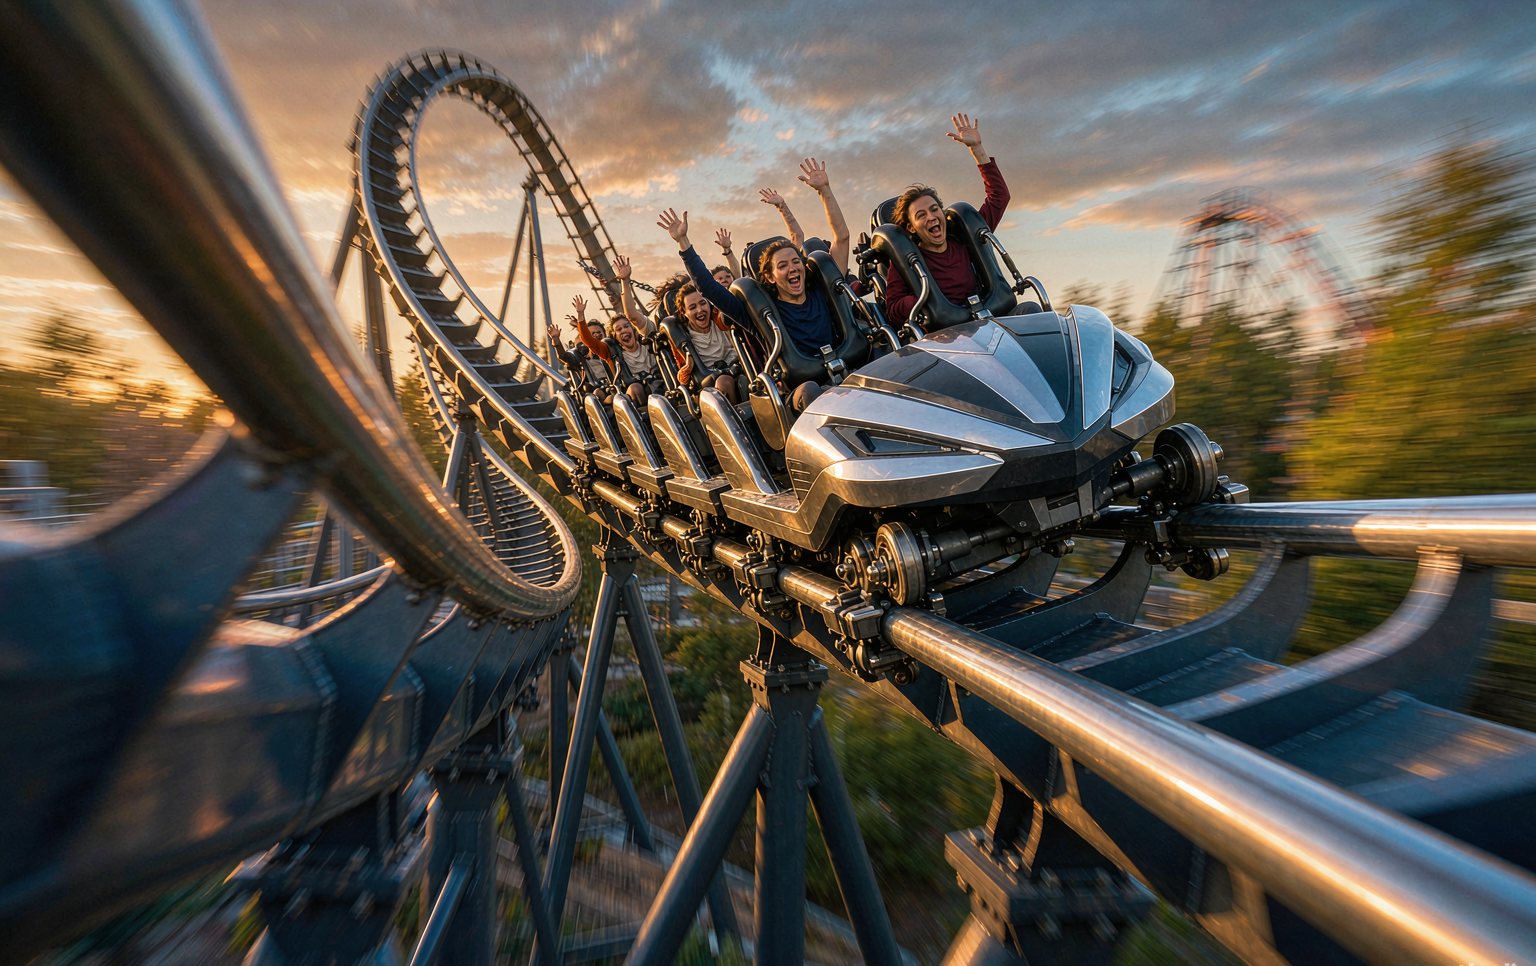
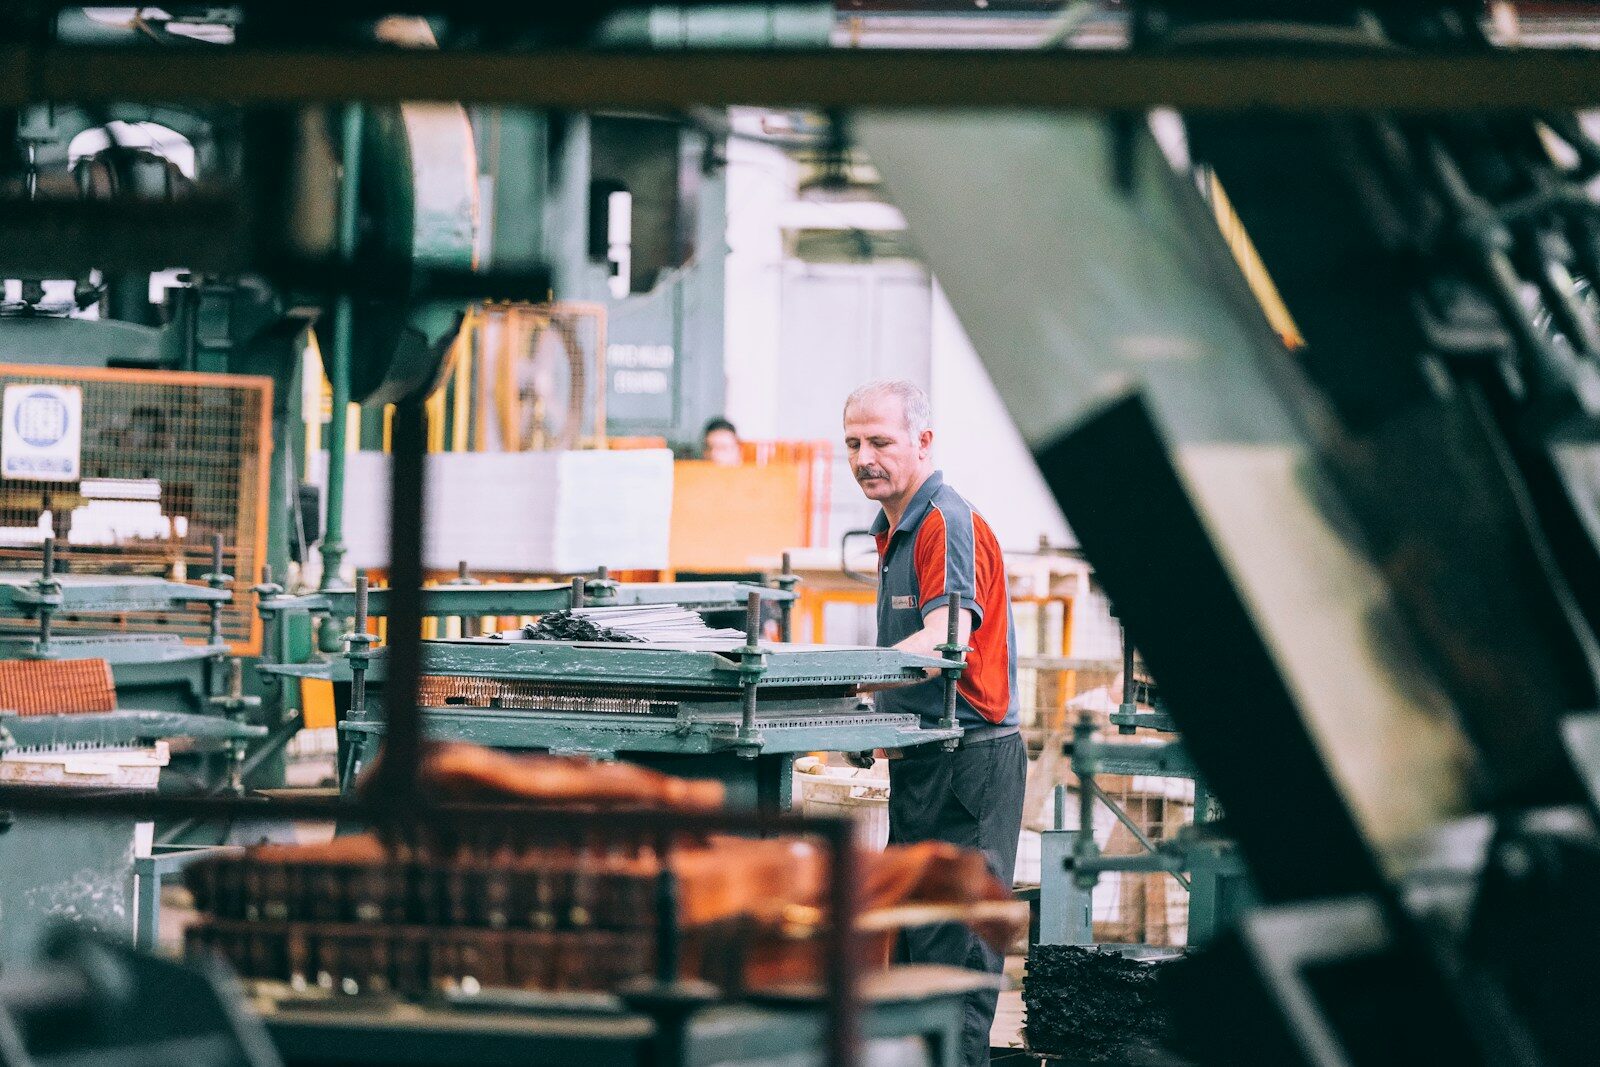
Fairground ride manufacturers operate at the intersection of heavy industrial fabrication and precision entertainment engineering. Unlike stationary installations, rides built for the traveling fairground circuit must be designed for repeated assembly and disassembly, transport on standard road vehicles, and reliable operation in variable environmental conditions. These requirements impose unique constraints on every aspect of the manufacturing process.
Design for Transport and Assembly
The defining characteristic that separates fairground ride manufacturers from their stationary-park counterparts is the transportability requirement. Every structural component must fit within standard shipping dimensions—typically 2.5 meters wide, 4.0 meters high, and 12-16 meters long for European road transport, or 2.6 meters wide and 16.7 meters long for North American oversize load permits.
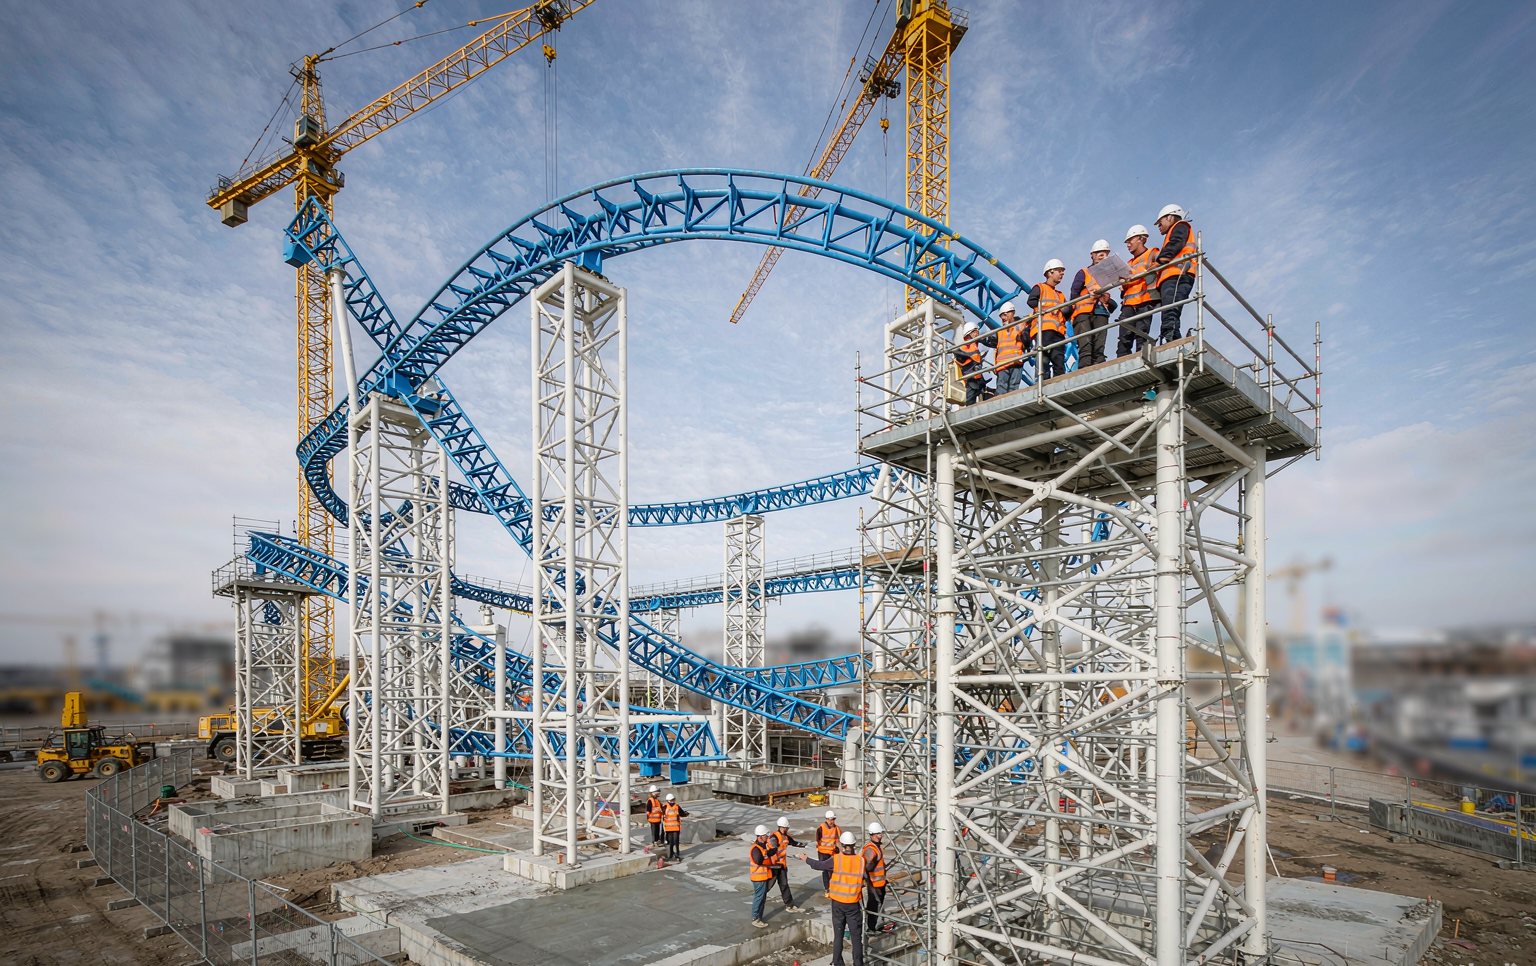
This constraint drives a modular design philosophy where the ride structure is broken into transportable sections connected by bolted flange joints. These joints use high-strength grade 10.9 or 12.9 hex bolts with controlled torque specifications, typically tightened to 70-80% of the bolt’s proof load. Each joint is equipped with locating pins or conical alignment features to ensure repeatable positioning accuracy within 0.5mm during reassembly.
Steel Fabrication Processes
The primary fabrication workflow at fairground ride manufacturers follows a standardized sequence:
- CNC plasma cutting: Structural plate components are cut from steel plate stock using computer-controlled plasma or fiber laser cutting systems. Tolerances of ±0.5mm are maintained on critical dimensions. Edge preparation for welding is performed simultaneously, creating bevel angles of 30-37.5 degrees for full-penetration weld joints.
- Roll forming: Tubular structural members are produced by cold-rolling flat plate through a series of progressive dies, followed by automated submerged arc welding (SAW) along the longitudinal seam. Standard tube diameters range from 168mm to 610mm for primary structural members.
- Machining: Critical interface surfaces, bearing housings, and shaft mounting points are machined on CNC horizontal boring mills or vertical machining centers. Tolerances of ±0.05mm are typical for bearing bores, with surface finish requirements of Ra 1.6 or better.
- Welding: All structural welding is performed by certified welders holding current EN ISO 9606-1 or AWS D1.1 certifications. Weld procedures are qualified to EN ISO 15614-1 standards, and every structural weld is documented with welder identification, procedure specification number, and inspection results.
- Surface treatment: After fabrication, components undergo shot blasting to SA 2.5 cleanliness standard, followed by a multi-coat paint system. The typical specification includes a zinc-rich epoxy primer (minimum 80 micrometers DFT), an epoxy intermediate coat (100-120 micrometers DFT), and a polyurethane topcoat (60-80 micrometers DFT) in the customer’s specified color scheme.
Quality Control and Testing Protocols
Fairground ride manufacturers maintain quality control programs that exceed standard industrial practice due to the life-safety nature of their products. Key quality checkpoints include:
- Material certification: Every batch of structural steel is supplied with EN 10204 Type 3.1 mill certificates verifying chemical composition and mechanical properties. Components are traceable from raw material heat number through to final installation.
- Weld inspection: 100% visual inspection of all structural welds, supplemented by non-destructive testing (NDT) on a minimum of 10% of critical welds using magnetic particle inspection (MPI) or ultrasonic testing (UT). Full-penetration welds in primary load paths receive 100% NDT coverage.
- Dimensional verification: After assembly of major sub-assemblies, critical dimensions are verified using total station theodolites or laser tracking systems with accuracy of ±1mm over 10-meter spans.
- Factory acceptance testing (FAT): Before shipment, each ride undergoes a complete operational test cycle at the manufacturer’s facility. This includes minimum 72 hours of continuous running for mechanical components, full-speed operation with weighted test dummies, emergency stop function verification, and control system fault injection testing.
Electrical System Manufacturing
The electrical control cabinets are assembled in dedicated clean-room environments to prevent contamination of sensitive components. Wiring follows IEC 60204-1 standards for machine electrical equipment, with color-coded conductors, ferrule-terminated connections, and comprehensive labeling. Cable harnesses for field wiring are pre-assembled on form boards to ensure consistent routing and connector alignment during on-site installation.
Safety-rated components including safety relays, safety-rated motor contactors, and emergency stop modules are sourced from certified suppliers and installed in segregated compartments within the control cabinet to prevent electromagnetic interference.
Documentation Packages
Fairground ride manufacturers provide comprehensive documentation packages with each installation, including structural calculation reports, electrical schematics, hydraulic and pneumatic circuit diagrams, parts catalogs with exploded-view illustrations, maintenance schedules, and operator training manuals. These documents are essential for regulatory compliance in most jurisdictions and form the basis for ongoing maintenance programs throughout the ride’s operational life.